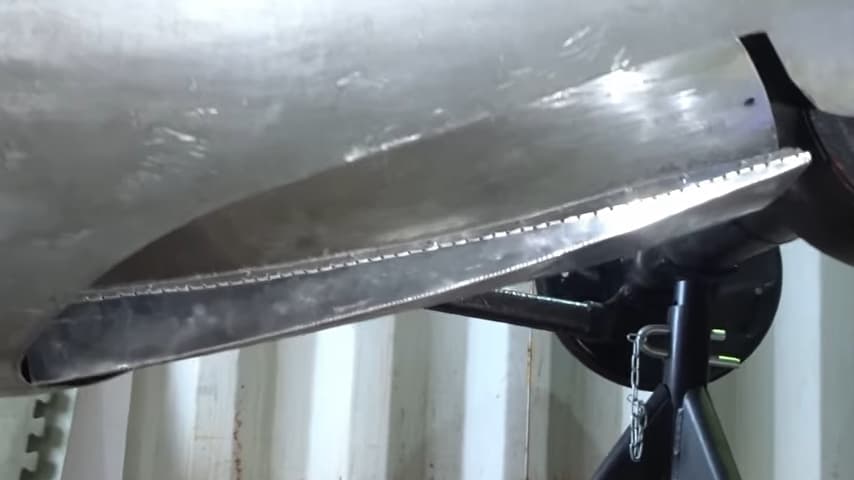
Drilling a line of small holes along a curved fold line lets you bend aluminum sheet metal cleanly, with no press brake, no slip roller, and no CNC. Fabricator John demonstrated the technique in episode 101 of his Belly Tank Lakester build series, using it to form a curved cosmetic exhaust splitter that follows the aerodynamic contours of a belly tank body, a shape with zero straight edges.
The hole-drilling method works because each perforation relieves stress at that point, letting the metal between holes bend rather than crack. John tested the obvious alternative first: cutting a shallow groove to create a pre-scored fold line. That failed. The grooved aluminum folded along the weakened line but cracked in the process. Holes do not crack. The finished part carries small perforations along every fold, but the piece mounts on the underside of the car and John reports they are invisible at normal viewing distance.
Skip to 7:55 in the embedded video to see the finished part. Watch from the beginning to understand the planning, layout, and incremental bending steps that make the result possible. The process is transferable to any compound-curve aluminum fabrication job where you have hand tools, a drill press, and time but no access to industrial forming equipment.
[READ ORIGINAL →]